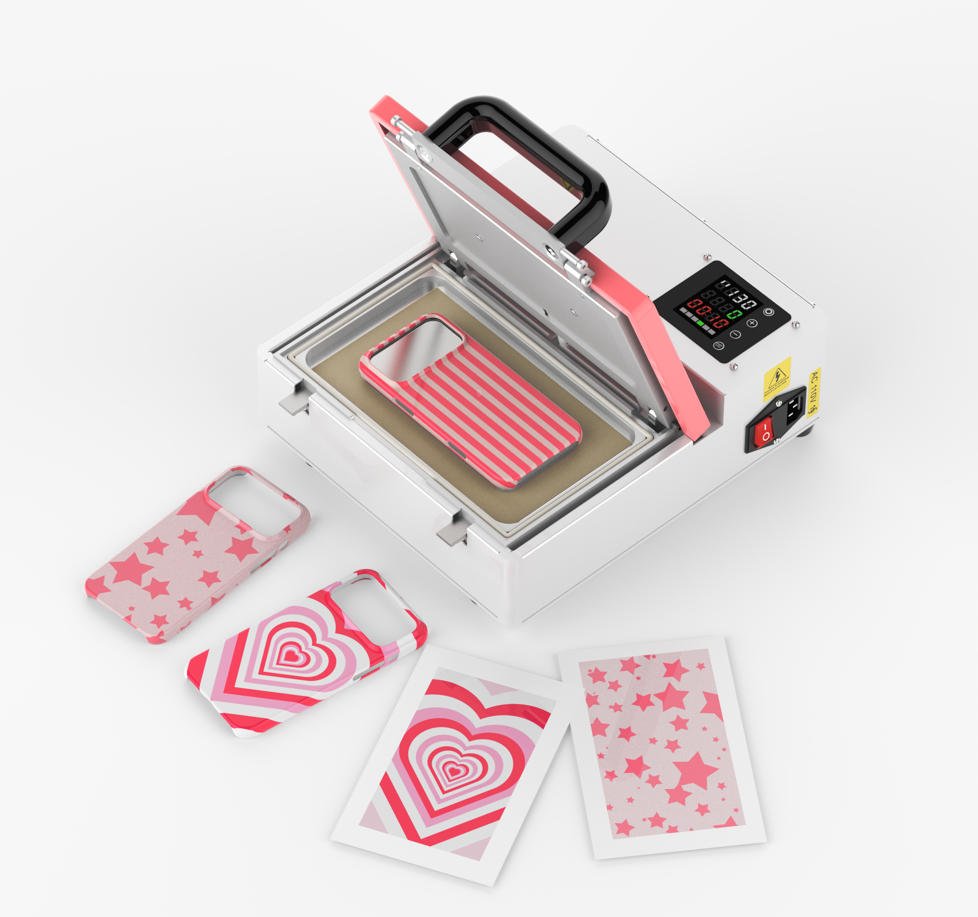
Contemporary brand competition no longer focuses solely on the functional aspects of products; amidst the trend toward market personalization, consumers now place even higher demands on a product’s visual packaging and aesthetic quality.
Whether for printed apparel from trendy sportswear brands, creative merchandise from cultural and creative sectors, or high-end corporate gifts, dye-sublimation printing is quietly displacing traditional screen printing and offset printing to become the preferred printing method for brands.
In essence, dye-sublimation printing precisely aligns with brands’ core demands for high quality, high efficiency, low cost, and eco-friendliness. Today, we will break down the fundamental logic behind brands’ preference for dye-sublimation printing.
1.Core Technology: Molecular-Level Penetration—Bidding Farewell to Traditional Printing Pitfalls.
The core of dye-sublimation printing lies in molecular penetration driven by high temperatures. Dye-sublimation ink is printed onto a transfer film; subsequently, under conditions of high heat and pressure, the ink sublimates into a gaseous state and permeates the interior of materials such as polyester or coated metals, where it permanently solidifies upon cooling.
The printed pattern becomes seamlessly integrated with the material itself through this molecular-level penetration, effectively preventing issues such as abrasion, peeling, and cracking.
2.Visual Texture: Cultivating High-End Differentiation.
For any brand, visual presentation serves as its primary competitive asset—and in this regard, the visual performance of dye-sublimation technology virtually eclipses that of traditional manufacturing processes.
1. Ultra-High-Definition Color Reproduction: This technology precisely replicates photo-realistic details—free of halftone dots or jagged edges—delivering a rich, vivid texture whether applied to the gradient team uniforms of sports brands or the high-resolution graphic designs found on cultural and creative products.
- Offering boundless design freedom, it supports full-surface curved coverage and breaks through the various limitations of traditional printing, allowing patterns to be displayed without any blind spots. Examples such as full-coverage printing on keycaps and 360-degree patterns on insulated mugs highlight the distinct advantages of dye-sublimation technology.
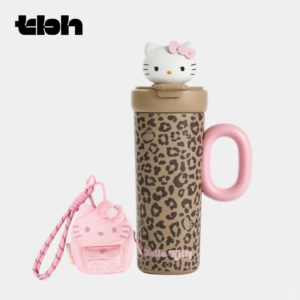
- Zero-Touch Experience: The printing process adds no perceptible thickness to the product, thereby preserving its original texture. Whether applied to sportswear, home textiles, or electronic accessories, it leaves absolutely no sensation of a foreign object—a feature that instantly elevates the product’s premium appeal.
3. Durability: Mitigating After-Sales Risks and Safeguarding Brand Reputation
Product durability is directly linked to a brand’s reputation, and the durability of sublimation printing surpasses that of conventional printing.
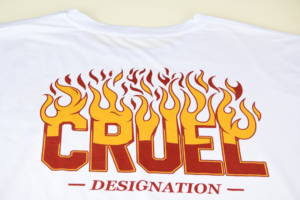
- shirts printed using sublimation technology maintain an exceptionally high level of color retention—remaining free from fading, bleeding, or peeling—even after more than 50 washes. When used outdoors, the print remains vibrant for 3 to 5 years; furthermore, during long-term storage, the colored areas will not discolor or become brittle. For brands, this translates to lower after-sales costs and helps prevent customer complaints regarding peeling prints or fading colors. The long-term durability of the product ultimately serves to strengthen user trust in the brand.
- 4.Production Flexibility: Aligned with Current Brand Needs
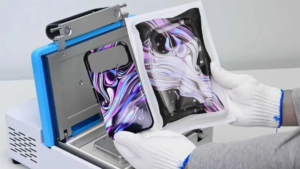
- Sublimation printing offers a minimum order quantity of just one item and is a fully digitized process; it requires no plate-making or screen exposure, resulting in zero setup fees. This method perfectly meets the small-batch production needs of brands—such as for trial products, limited editions, and promotional merchandise—while avoiding the high costs typically associated with traditional printing. 2. Lightning-fast delivery: the process flows seamlessly from design to printing, transfer, and final product. Leveraging Zhuode Industry’s proprietary consumables, we can produce and deliver samples on the very same day. This represents a multi-fold increase in efficiency compared to the 3–7 day plate-making cycle of traditional printing, enabling us to rapidly fulfill urgent and last-minute orders.
- Compatible with a full range of product categories—accommodating both soft goods (apparel, bags, pillowcases) and hard goods (thermos mugs, phone cases, keychains). This allows brands to span multiple product lines, thereby reducing procurement costs.
5.Cost: A Long-Term Advantage Driving Sustainable Brand Growth
Sublimation printing is not limited solely to small-batch production; from a long-term perspective, its overall cost structure offers distinct advantages. Traditional printing methods entail high plate-making fees, requiring the creation of entirely new plates whenever a design changes—resulting in significant sunk costs. In contrast, sublimation printing incurs no plate-making fees, and its per-unit cost remains stable; whether producing a single item or a batch of 1,000, the unit price remains remarkably consistent.
Crucially, it ensures environmental compliance: the entire sublimation process generates zero wastewater discharge. The inks feature an eco-friendly, water-based formulation that meets the EU REACH international standard, thereby facilitating brands’ entry into overseas markets and helping them mitigate environmental risks.
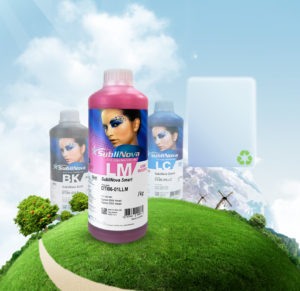
6.Printing Case Studies: Sublimation Printing Across Product Categories
Sports brands utilize sublimation to produce team uniforms and training apparel, resulting in breathable, durable garments with a premium feel. Cultural and creative brands employ it to craft printed merchandise—such as fridge magnets and keychains—thereby achieving complete creative freedom in their designs. Corporate entities leverage it to customize business gifts, ensuring rapid delivery and a consistent brand image. Finally, home goods and digital accessory brands use this technique to elevate the perceived quality of their products, effectively catering to users’ demands for personalization.
In summary: For brands, choosing sublimation printing is never merely a matter of selecting a printing technique; rather, it represents a choice for quality and efficiency, cost-effectiveness, and long-term growth.
Prosub is a consumables supplier with 15 years of experience in sublimation printing. We offer comprehensive, one-stop sublimation solutions—encompassing market trend consulting, technical process guidance, equipment installation and commissioning, and the supply of consumables. From initial product selection and implementation to post-sales support, a dedicated specialist will personally oversee every step of the process. We invite you to contact us to obtain your customized sublimation solution!