As a specialized source supplier of sublimation consumables—integrating R&D, manufacturing, sales, and custom processing—Prosub consistently adheres to international production standards. Boasting an extensive product portfolio and a comprehensive suite of export certifications—including ISO, CE, RoHS, FCC, and others—we are able to provide domestic and international clients with high-quality, fully compliant blank sublimation consumables suitable for export.
1.Comprehensive Range of Consumables: Continuously Iterating New Products to Meet Market Demand
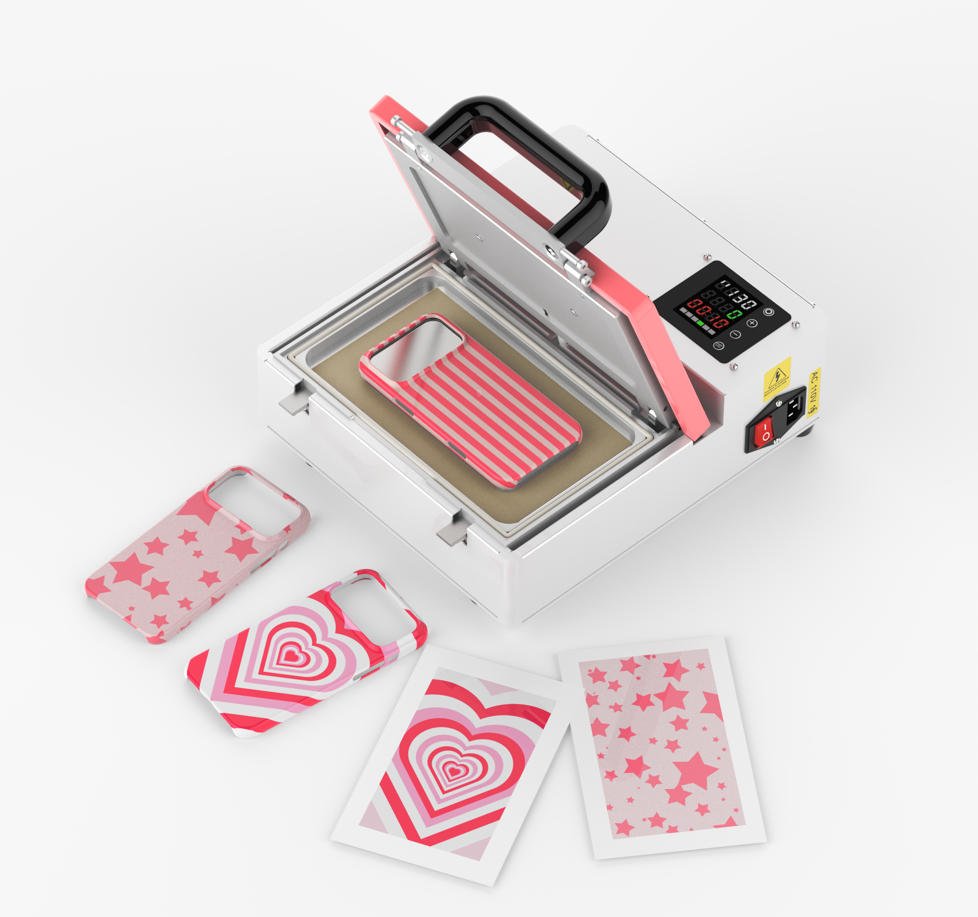
Prosub boasts an extensive matrix of over 8,000 types of blank consumables, comprehensively covering customization scenarios across a wide range of sectors. In the realm of 3C digital accessories, our core offerings include various blank substrates—such as sublimation-ready phone cases, computer cases, and keycaps. These products are compatible with most mainstream device models; featuring flat, uniform surfaces, they deliver exceptional color reproduction during thermal transfer printing and are highly resistant to deformation and fading, thereby fully meeting the demands for personalized digital customization.
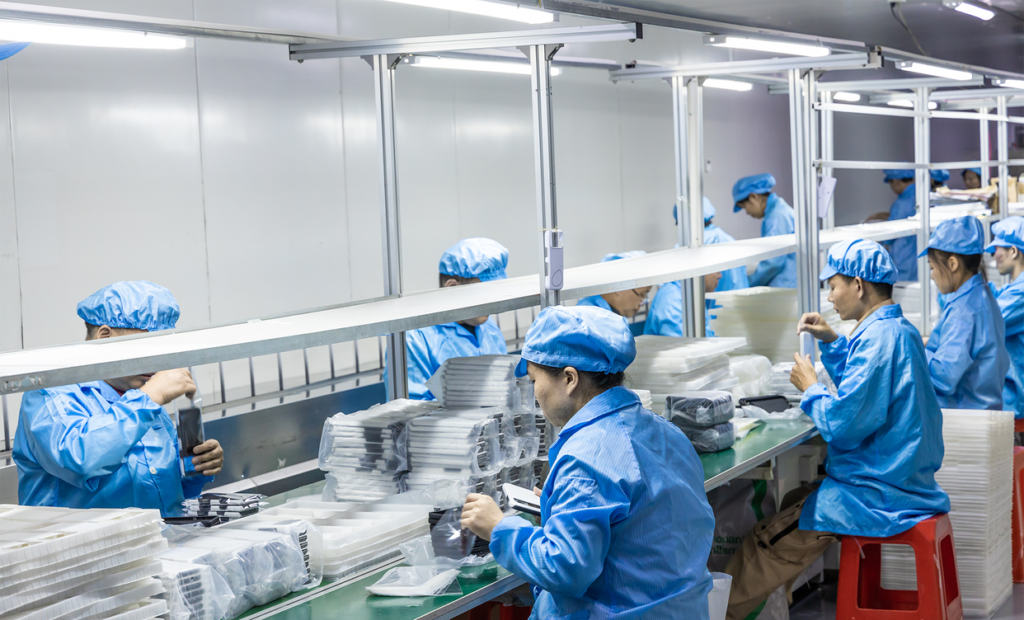
At the same time, our product portfolio extends across various sectors of daily consumer life—encompassing a diverse range of consumables such as apparel, home décor, and pet supplies—and is adaptable to a wide array of sublimation processing scenarios, including garment printing, home decoration, and the creation of personalized pet accessories.
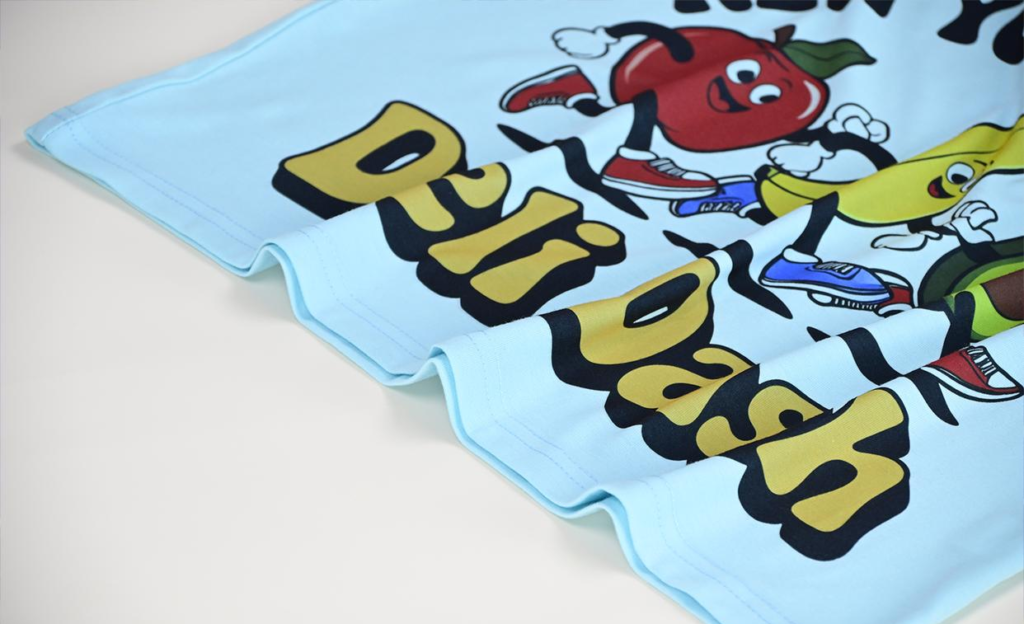
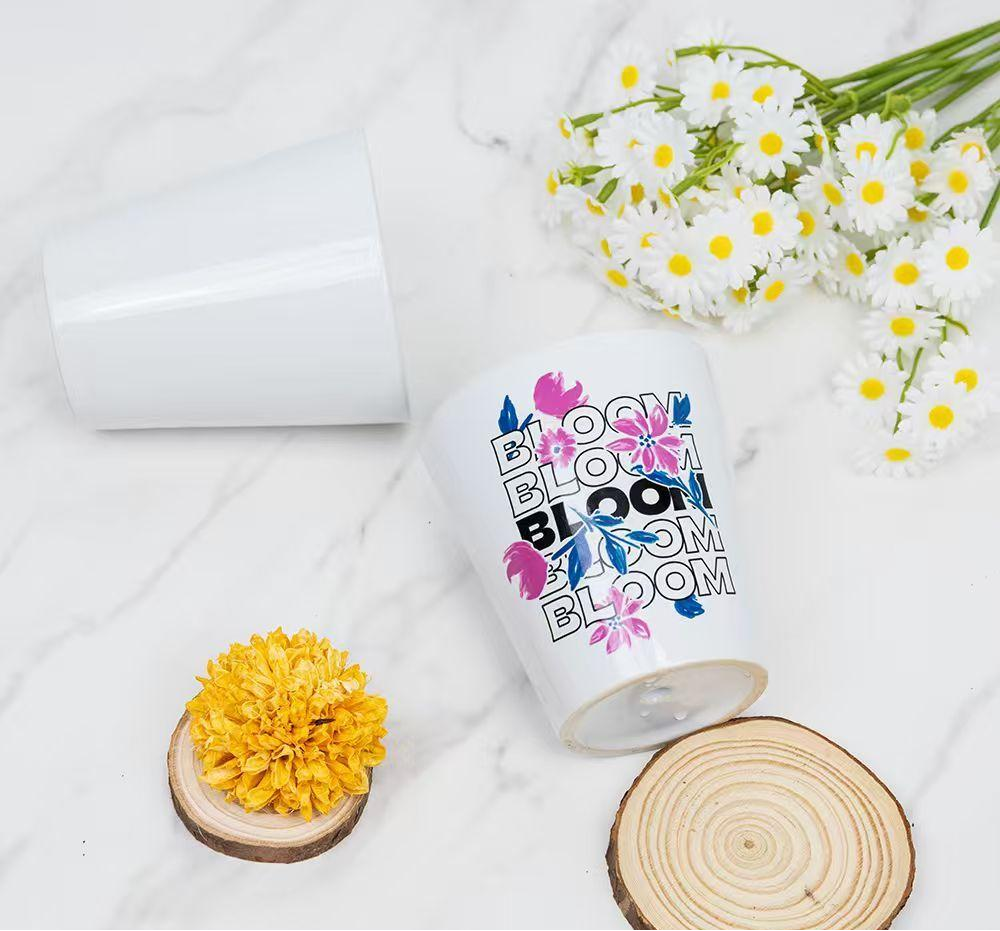
Backed by a professional R&D team, we continuously invest in the development of new products and iterative upgrades. By constantly enriching our product categories and optimizing manufacturing processes, we consistently supply the market with differentiated, high-quality sublimation consumables, thereby empowering our clients to seize market opportunities.
2. Integrated Industrial Services: Consumables Supply and Outsourced Processing
Prosub possesses comprehensive industrial service capabilities, having established an integrated service model encompassing R&D, production, sales, and outsourced processing.
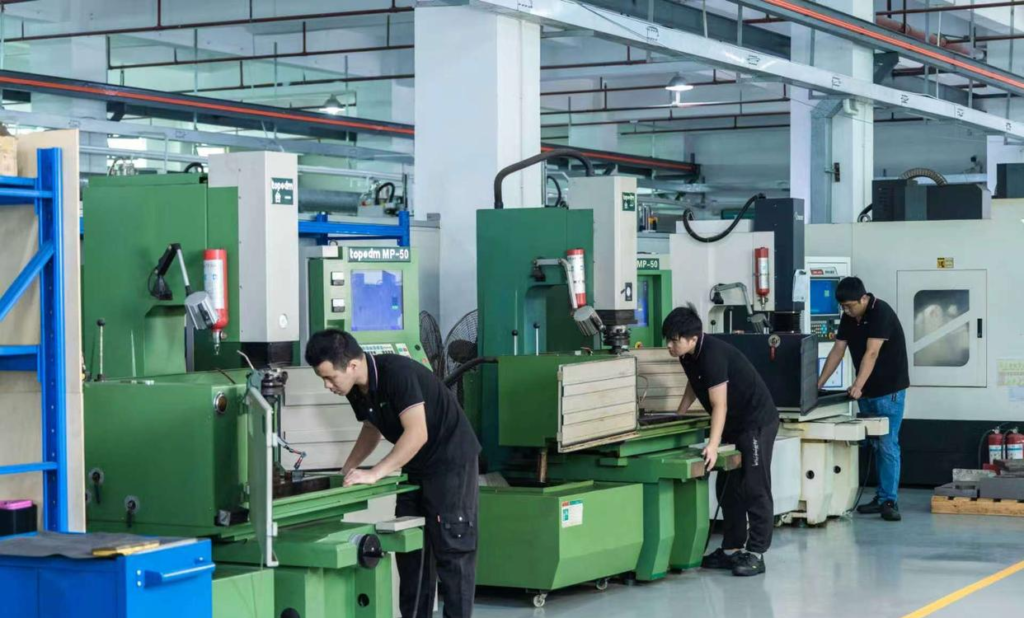
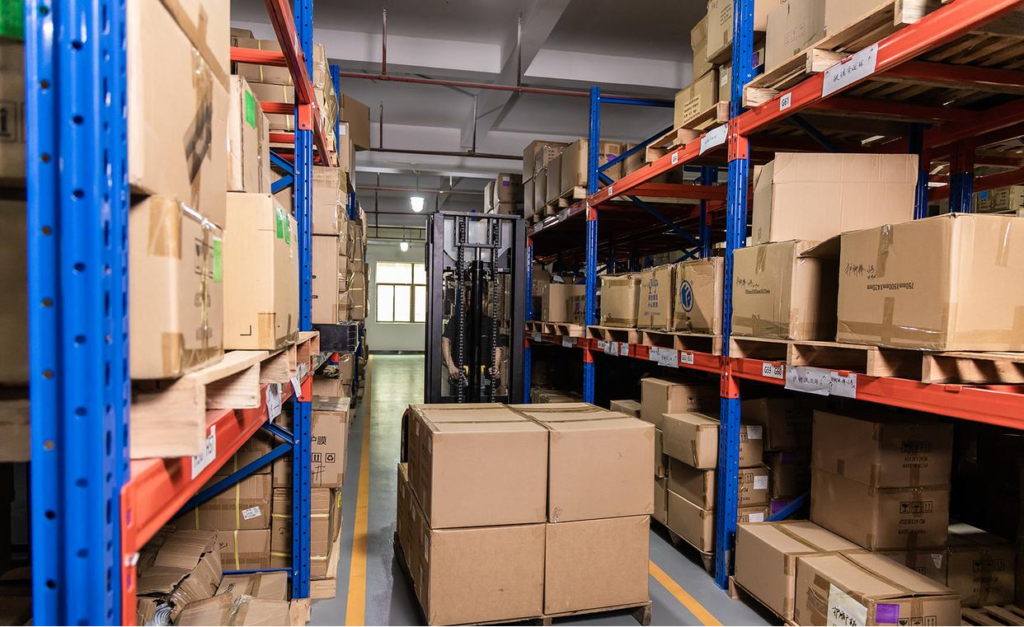
Our proprietary factory is equipped with mature, standardized production lines that enable us to maintain full autonomous control over the entire process—from raw material selection, manufacturing, and finished product inspection to warehousing and shipping. This capability allows us to ensure a stable supply of large-volume stock while also enabling us to customize exclusive consumable products tailored to our clients’ specific requirements.
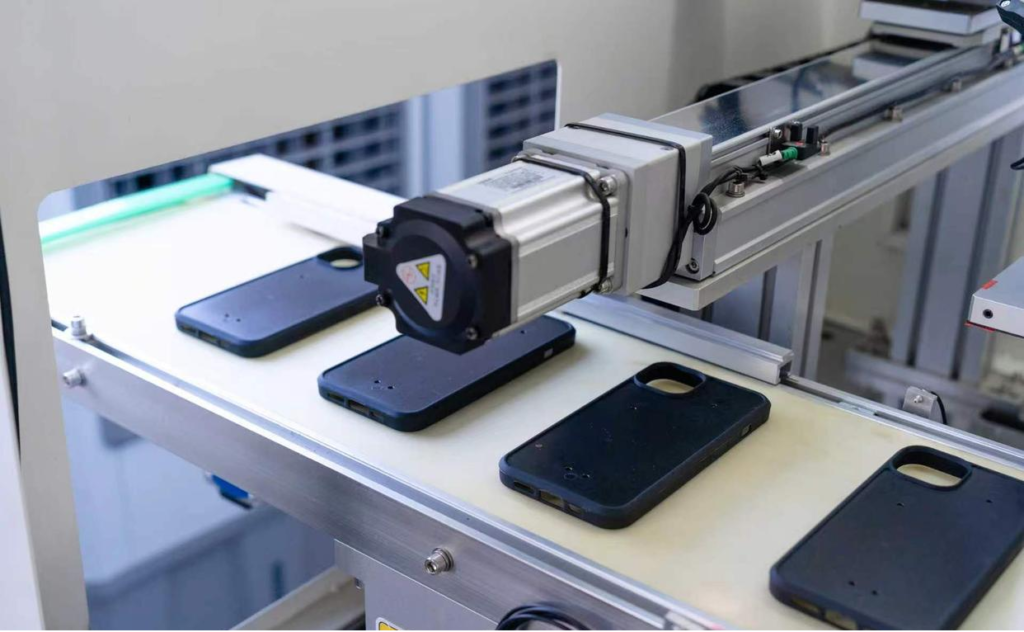
Concurrently, Prosub undertakes various outsourced processing services, providing clients with a one-stop solution for dye-sublimation processing. By eliminating the cumbersome procedures associated with intermediary coordination, we reduce operational costs and accommodate a diverse range of collaboration models—from small-to-medium batch customization to large-scale export orders.
3.Complete Set of International Export Certifications, Compliant with Overseas Market Standards
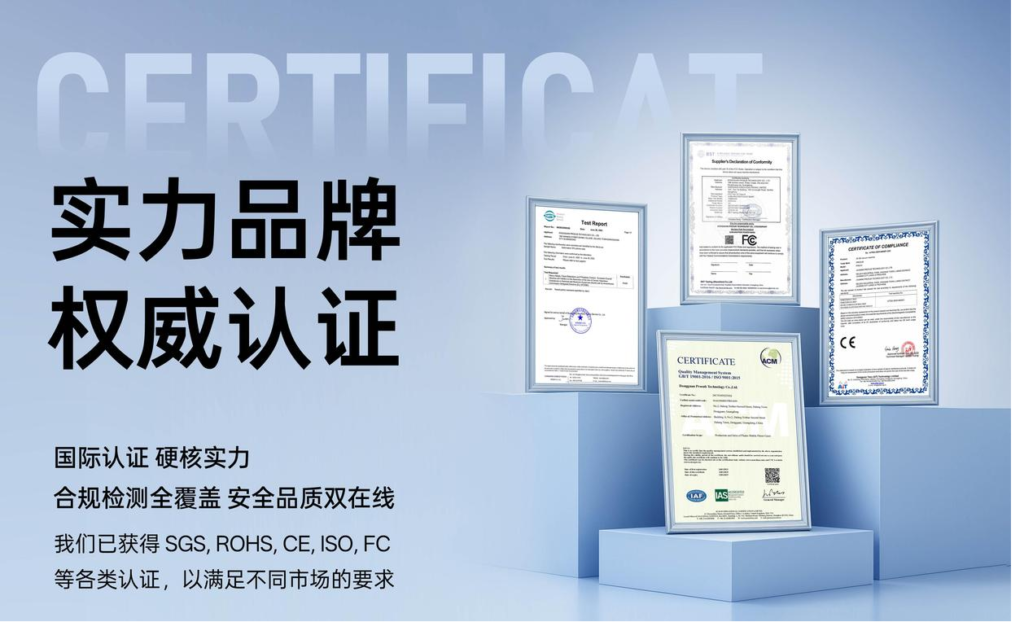
Over the years, Prosub Industrial has cultivated a diverse client base spanning numerous domestic and international markets. To comprehensively address our clients’ export compliance challenges and ensure alignment with overseas market access standards, we place paramount importance on international product certification. By proactively benchmarking against European and globally recognized trade standards, we have successfully obtained a wide range of international certifications—including ISO, CE, RoHS, and FCC—thereby establishing a robust export certification framework that lays a solid foundation for the smooth export of our products.
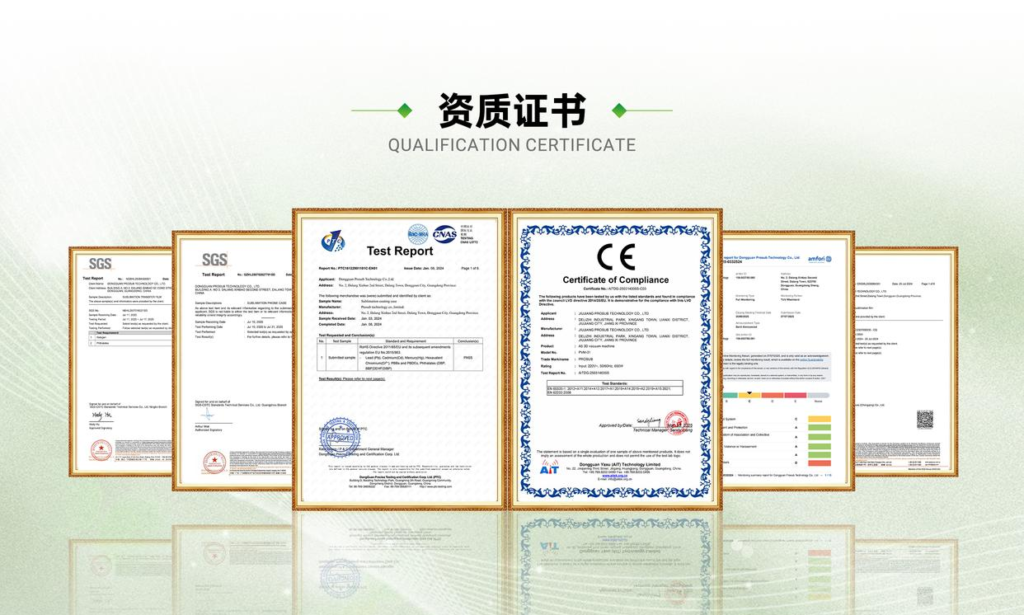
4. Backed by Authoritative Certifications: Unlocking Access to Global Markets
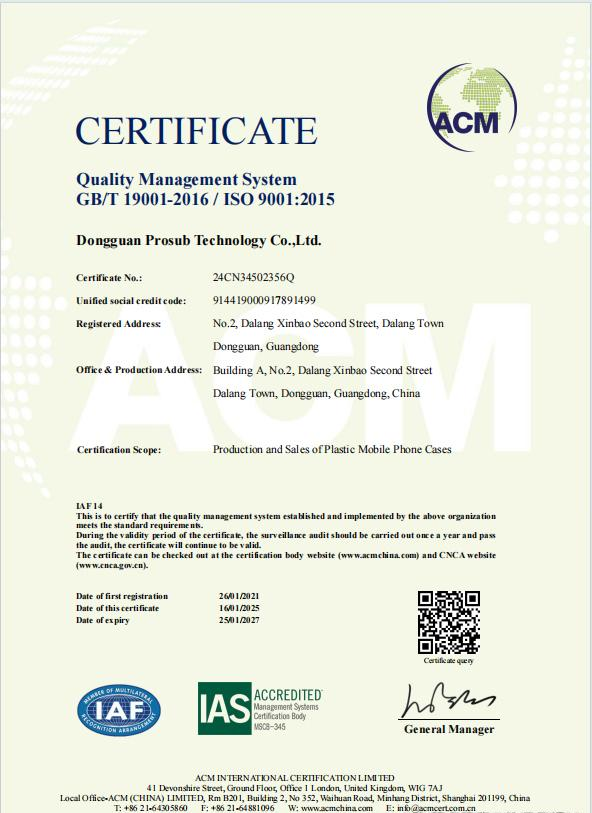
Our ISO system certification standardizes our company’s entire production, management, and quality control processes. It serves as proof that our production models, management systems, and quality control measures meet international standards, enabling us to consistently and reliably deliver high-quality products.
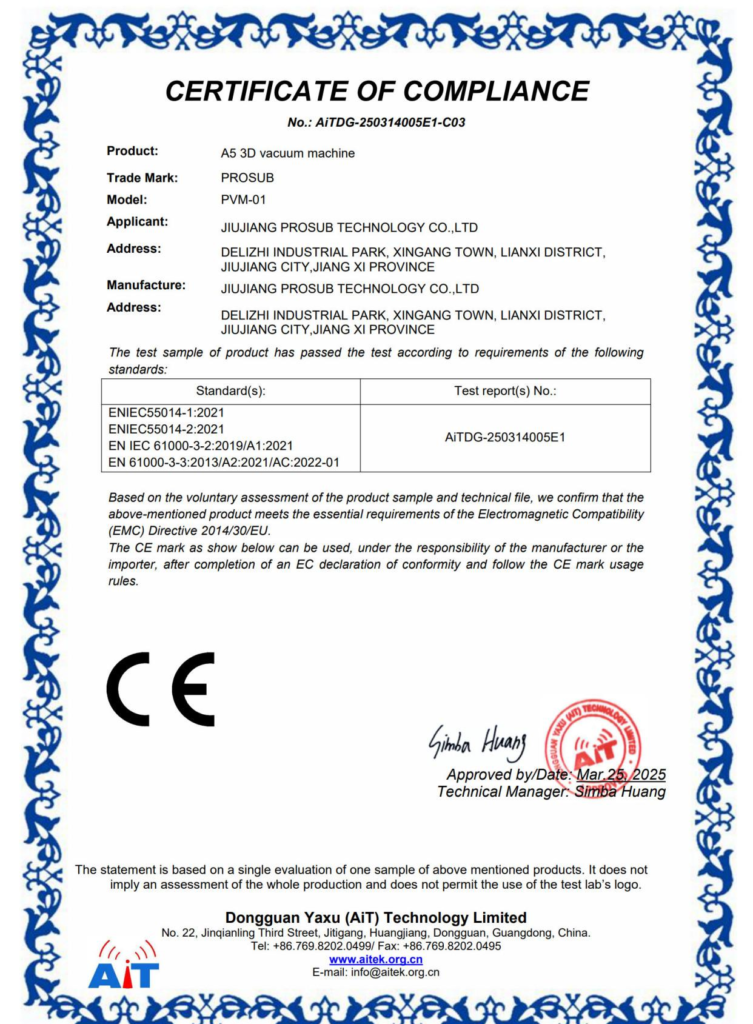
As a mandatory safety certification for the EU market, CE certification serves as the “passport” for products entering Europe; it signifies that our dye-sublimation consumables fully comply with the EU’s rigorous market entry standards across key indicators such as safety, health, and environmental protection.
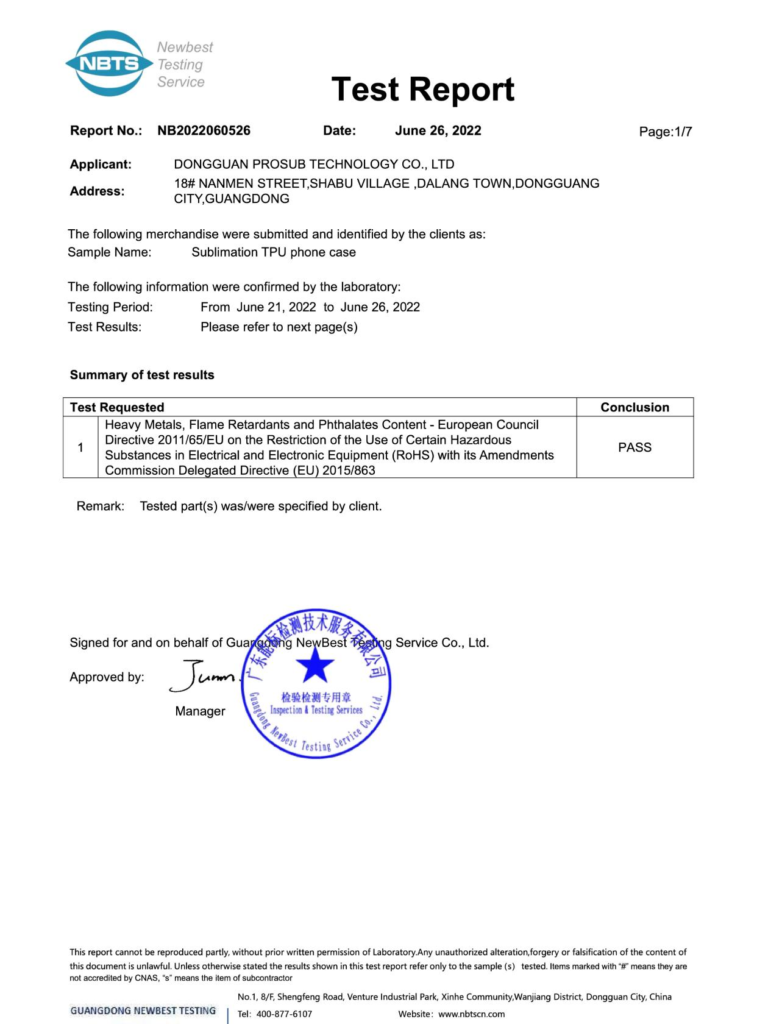
The RoHS environmental certification prioritizes the environmental performance of products, strictly limiting the content of hazardous substances—such as lead, mercury, and cadmium—to ensure that products are eco-friendly, non-toxic, and harmless. This aligns with global trends in green trade and fully satisfies the safety requirements of end consumers overseas.
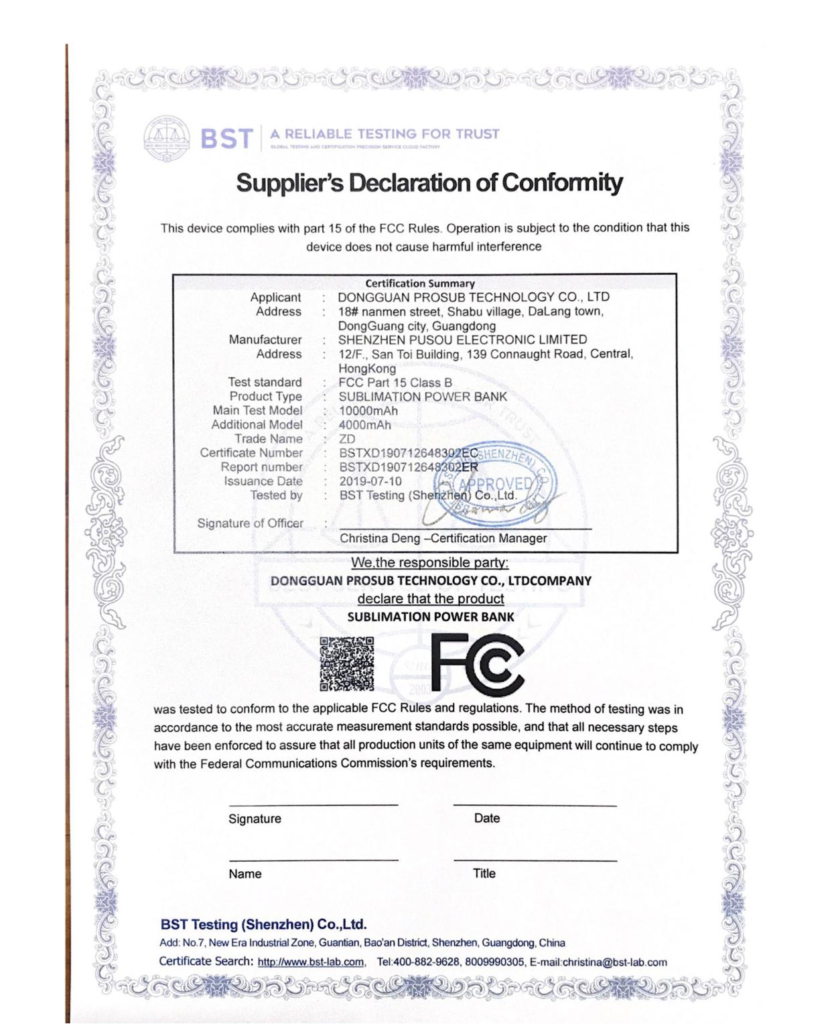
FCC certification is a certification issued by the U.S. Federal Communications Commission. It addresses the electromagnetic compatibility and radio frequency safety of electronic products, ensuring that “3C-category blank consumables”—such as magnetic phone cases and power banks—comply with the electromagnetic radiation and interference suppression requirements of the U.S. and North American markets, thereby facilitating their smooth clearance into the North American market.
Backed by a comprehensive suite of authoritative certifications, our dye-sublimation products can effortlessly clear customs for export and successfully enter major markets across Europe and the globe. This eliminates the need for clients to navigate complex, additional compliance procedures, thereby significantly enhancing the efficiency of international trade collaborations.
5. Summary of Core Strengths: Compliance and Quality Empower Global Collaboration
From regulatory certification to the practical implementation of quality control, and from product innovation to service enhancements, we consistently place the needs of our global clientele at the very core of our operations. Through standardized, compliant, and high-quality products and services, we have established a premier supply chain for dye-sublimation consumables.
Our comprehensive suite of international export certifications, rigorous end-to-end quality control, extensive product portfolio, and seamless integrated services constitute not only our core competitive advantages but also our solemn pledge to every client, both at home and abroad.